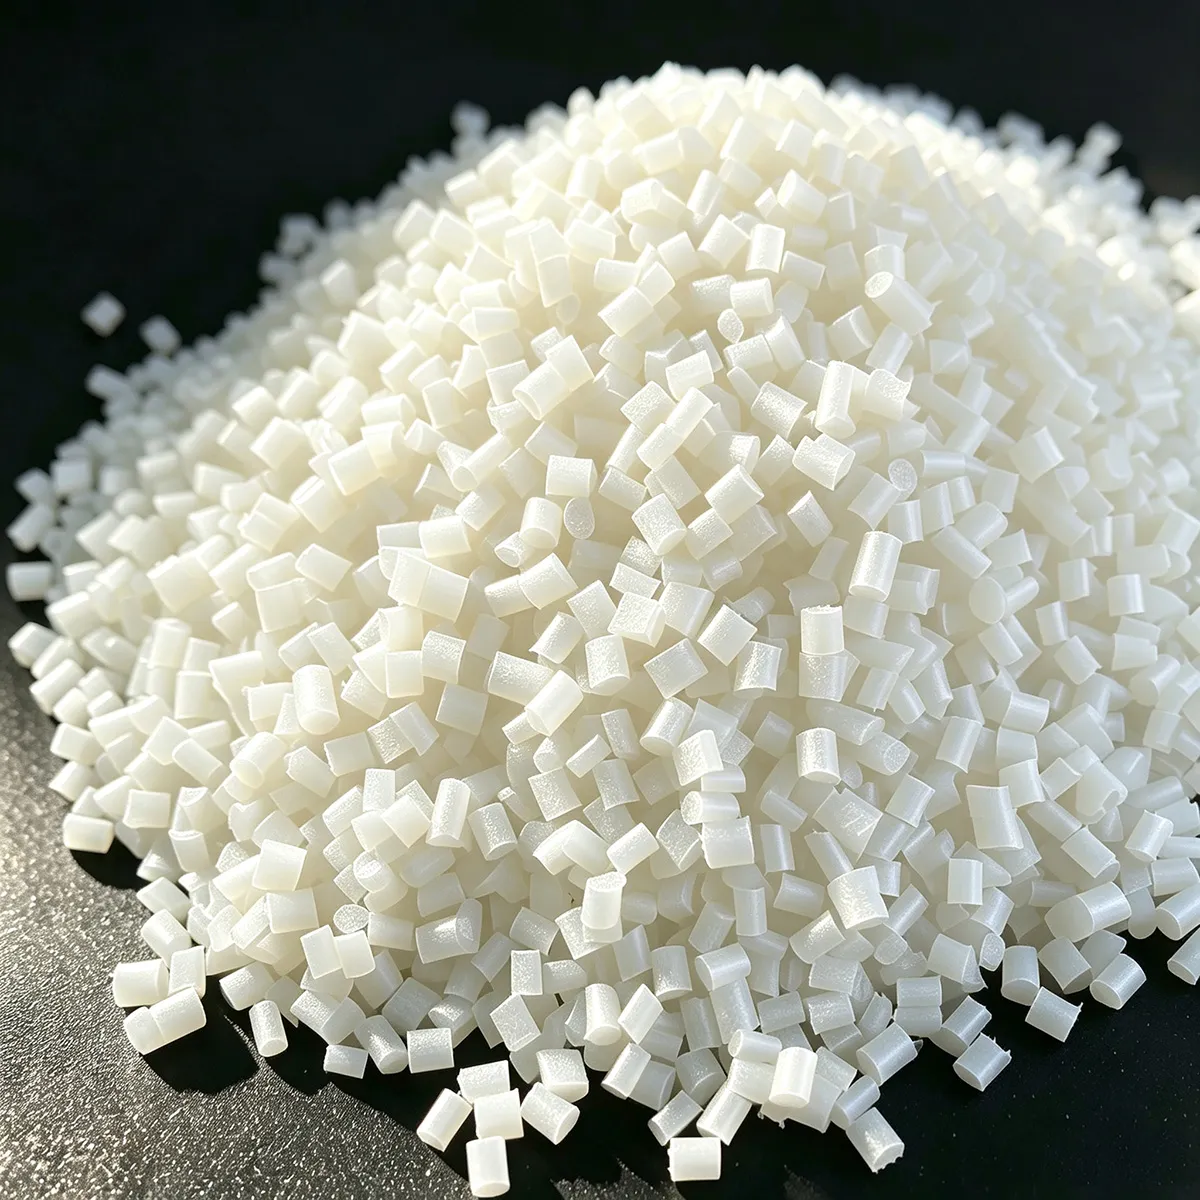
Modified Nylon PA6 · Economy Grade
PA6 GBA35 · 35% Glass Fiber Reinforced Economy Nylon 6 Pellets
Economical PA6 compound reinforced with 35% chopped glass fiber. Balanced cost-performance grade offering 138 MPa tensile strength and 15 kJ/m² notched Izod impact. Excellent choice for industrial structural brackets, pulleys, handles and general load-bearing components without the premium cost of higher-tier resin.
| Tensile Strength (ISO 527) | 138 MPa |
|---|---|
| Flexural Modulus (ISO 178) | 6,900 MPa |
| Notched Izod Impact @ 23°C | 15 kJ/m² |
| HDT @ 1.82 MPa | 195 °C |
| Density | 1.36 g/cm³ |
| MVR @ 275°C / 5 kgf | 35 cm³/10 min |
| Shrinkage (Flow / Cross) | 0.35% / 0.95% |
| Certifications | ISO 9001, ROHS 2.0, REACH |
Product Overview & Key Features
PA6 GBA35 is an engineering plastic compound produced by Juhai Plastics using a high-value PA6 base resin reinforced with 35% high-quality silane-sized chopped E-glass fibers compounded on our co-rotating twin-screw extrusion line. The high fiber content provides significant stiffening and mechanical reinforcement, while our optimized fiber-sizing chemistry ensures excellent resin-fiber interfacial adhesion — delivering mechanical retention levels close to premium-grade equivalents at an 18-22% lower price point.
Core Performance Advantages
High Specific Strength: 35% glass fiber loading gives tensile modulus of 7,800 MPa — three times stiffer than unreinforced PA6 — suitable for medium-to-high load structural components.
Balanced Cost vs. Performance: Economy base resin with premium-grade glass fiber delivers 90%+ of premium PA6 GF30 mechanicals at a significantly lower material cost.
Good Heat Resistance: HDT of 195°C at 1.82 MPa allows continuous use at elevated temperatures typical in under-bonnet non-critical automotive parts, industrial machinery near motors, and heat-generating electronics housings.
Excellent Processability: Controlled MVR of 35 cm³/10 min gives flow characteristics well adapted to both thin-wall and thick-wall injection molding. Low plate-out and consistent color batch-to-batch.
Optimized Value: Using our in-house optimized formulation reduces per-part material cost without sacrificing critical mechanical properties. High-CTI 400V / 600V formulation options available on request for electrical connector applications.
Recommended Applications
Industrial Machinery
Structural brackets, bearing cages, pulleys, idlers, gears, pump housings, wear pads.
Automotive (Non-Safety)
Secondary engine bay brackets, HVAC housings, cable ties, fasteners, inner door components.
Electrical & Electronics
Non-halogen-free electrical bobbins, connector backshells, relay bases, terminal blocks.
Power & Garden Tools
Tool inner frames, support brackets, gear housings, lawn mower and trimmer structural parts.
Home & Consumer
Appliance structural frames, furniture hardware, sports goods, kitchen appliance inner parts.
General Injection Molding
Any medium-load injection molded part where stiffness, heat and cost balance is required.
Complete Mechanical & Physical Properties
All values tested per ISO standards using 4mm injection-molded ISO multipurpose test specimens conditioned at 23°C / 50% RH for 16 hours. Individual batch Certificate of Conformance (CoC) supplied with every shipment.
Mechanical Properties
| Property | Test Standard | Value |
|---|---|---|
| Tensile Strength | ISO 527 | 138 MPa |
| Tensile Modulus of Elasticity | ISO 527 | 7,800 MPa |
| Elongation at Yield | ISO 527 | 2.5 % |
| Elongation at Break | ISO 527 | 2.8 % |
| Flexural Strength | ISO 178 | 215 MPa |
| Flexural Modulus | ISO 178 | 6,900 MPa |
| Notched Izod Impact (1A), 23°C | ISO 180 | 15 kJ/m² |
| Unnotched Izod Impact (1U), 23°C | ISO 180 | 68 kJ/m² |
| Charpy Notched Impact (1eA), 23°C | ISO 179 | 12 kJ/m² |
| Rockwell Hardness (R Scale) | ISO 2039-2 | R 112 |
Thermal Properties
| Property | Test Standard | Value |
|---|---|---|
| Heat Deflection Temperature (@ 1.82 MPa) | ISO 75/Af | 195 °C |
| Heat Deflection Temperature (@ 0.45 MPa) | ISO 75/Bf | 208 °C |
| Vicat Softening Temp (B/50) | ISO 306 | 212 °C |
| Melting Peak (DSC) | ISO 11357 | 221 °C |
| Coefficient of Linear Thermal Expansion | ISO 11359-2 | 3.2 × 10⁻⁵ °C⁻¹ (flow dir.) |
| Continuous Use Temperature (UL 746B, Electrical) | UL 746B | 115 °C (evaluated) |
Physical, Processing & Other
| Property | Test Standard | Value |
|---|---|---|
| Density | ISO 1183 | 1.36 g/cm³ |
| Melt Volume-Flow Rate (MVR) 275°C, 5.0 kgf | ISO 1133 | 35 cm³/10 min |
| Mold Shrinkage — Flow Direction | ISO 294-4 | 0.35 % |
| Mold Shrinkage — Cross Direction | ISO 294-4 | 0.95 % |
| Water Absorption (24 h, 23°C immersion) | ISO 62 | 1.00 % |
| Surface Resistivity | IEC 60093 | 1 × 10¹⁵ Ω/sq |
| Volume Resistivity | IEC 60093 | 1 × 10¹⁴ Ω·cm |
| Dielectric Strength (short-time, 2 mm) | IEC 60243-1 | 19 kV/mm |
| Comparative Tracking Index (CTI) | IEC 60112 | CTI 1 (≥ 600 V) |
Processing & Handling Guidelines
Injection Molding Parameters
| Process Parameter | Recommended Range | Notes |
|---|---|---|
| Pre-Drying | 80 °C × 4 hours; to < 0.08% moisture | Dehumidifying dryer mandatory. Ambient air drying is not sufficient. |
| Barrel Temp — Rear / Middle / Front | 235 °C / 250 °C / 265 °C | Gradual temperature profile; avoid excessive rears to prevent GF breakage. |
| Nozzle Temperature | 260 - 270 °C | Slightly lower than front zone to prevent drooling. |
| Mold Temperature | 60 - 90 °C | 80°C+ recommended for optimal GF impregnation and part surface finish. |
| Injection Pressure | 80 - 130 MPa | Depends on wall thickness; thin walls may need higher. |
| Holding Pressure | 60 - 80% of injection pressure | Holding time: 10-25 s depending on wall thickness. |
| Screw Back-Pressure | 5 - 10 bar | Higher back-pressure improves GF dispersion but increases fiber breakage. |
| Screw Speed (RPM) | 80 - 150 rpm | Moderate speed minimizes fiber attrition and shear heating. |
Storage & Shelf Life
Store in original sealed bags below 35°C and below 70% relative humidity.
Keep away from direct sunlight and sources of heat or open flame.
Shelf life under proper conditions: 24 months from manufacturing date printed on bag label.
Once opened, use contents within 4 weeks or re-seal with desiccant.
Packaging, Shipping & MOQ
| Standard Packaging | 25 kg heat-sealed kraft / PE composite bag with inner aluminum moisture barrier |
|---|---|
| Pallet Configuration | 40 bags per standard export pallet = 1,000 kg (1 MT) per pallet; stretch-wrapped with corner protectors |
| MOQ (Minimum Order Quantity) | 1,000 kg (1 full pallet / 40 bags). Smaller 100 kg trial batches available on request. |
| Stock Lead Time | 3-5 working days after receipt of payment (ex-works Ningbo) |
| Custom Color / Custom Formulation MOQ | 5,000 kg (5 pallets) |
| 20 ft FCL Loading | ~ 20,000 kg (20 pallets of 1 MT) |
| 40 ft HC FCL Loading | ~ 27,000 kg (27 pallets of 1 MT) |
| Documentation Provided | Commercial Invoice, Packing List, Bill of Lading / AWB, Certificate of Origin, CoC (Test Report), ROHS / REACH compliance letter, MSDS on request. |
Request Custom Quote, Sample or Datasheet
Fill in the form below for PA6 GBA35 or any other grade. Our technical sales engineer will contact you within 24 hours with datasheet, pricing, shipment lead time and sample availability. Free 2 kg samples available for genuine evaluation purposes (freight collect for international).